Skip to content

Superior Quality, Superior Production

000
Kandahar, Afghanistan

Steel thatholds thesouth together.

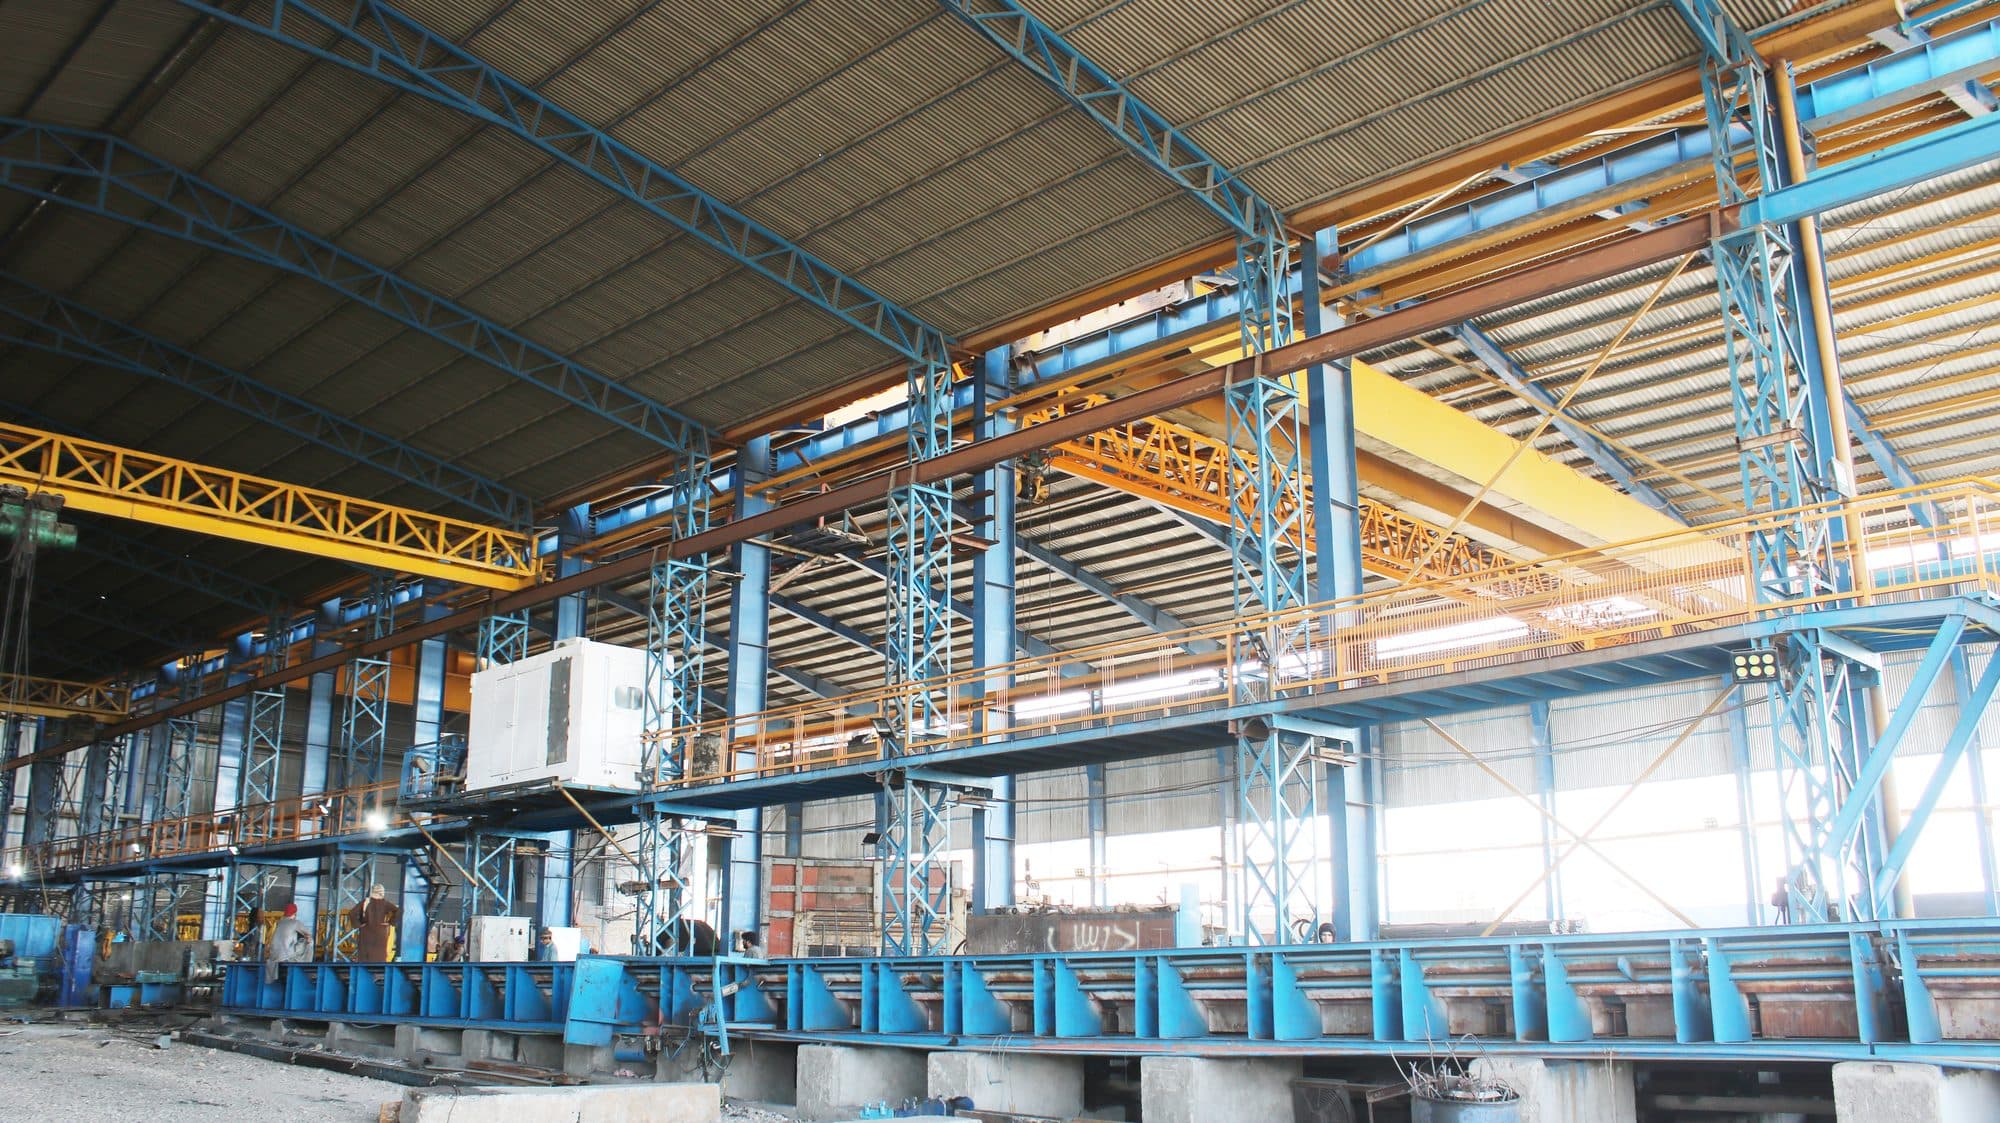
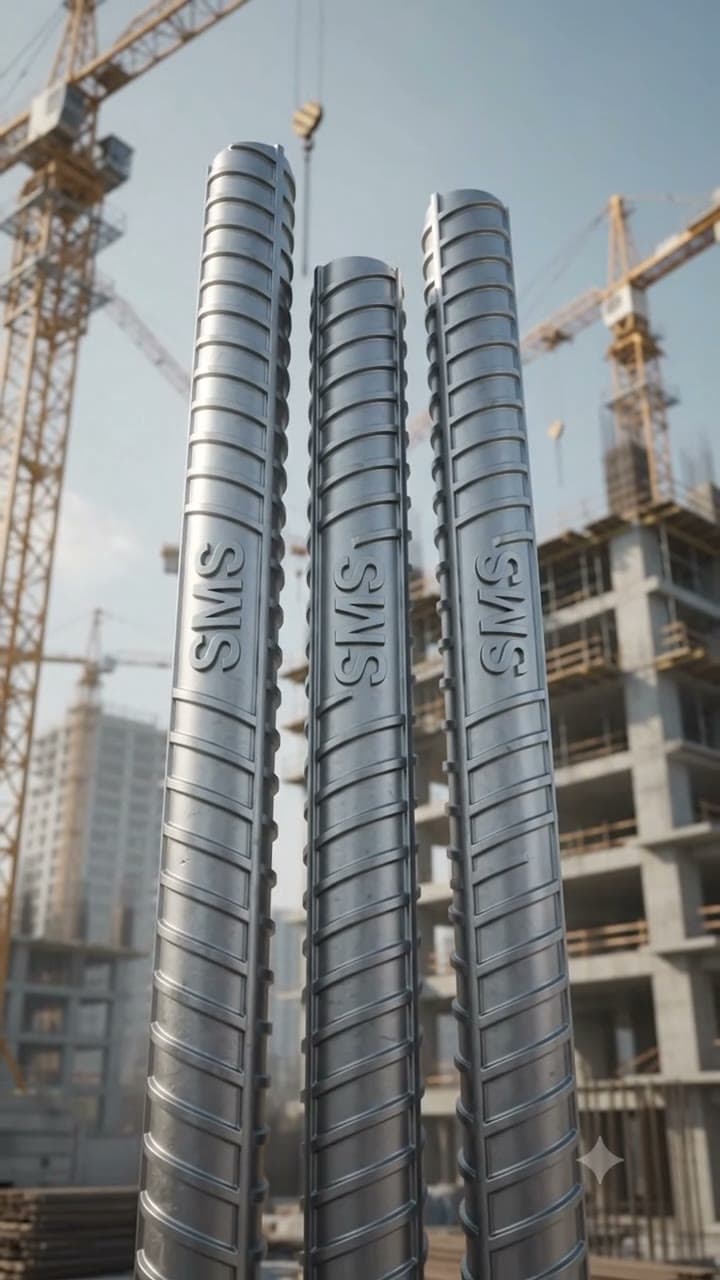
Shams Madina Steel Mill melts, rolls and tests reinforcement bar and structural sections at Shorandam Industrial Park. Four ISO certifications, two in-house laboratories, and a roll mark on every bar we ship.

Standard
ASTM A615
Grade
G60+
Rebar
8–32 mm
Length
11.7 m

Line status

Running

Scrap yardMelt shopCasterRolling millDispatch
  1. 01Scrap yard
  2. 02Melt shop
  3. 03Caster
  4. 04Rolling mill
  5. 05Dispatch
ASTM A615 / A370AASHTO M31MISO 9001:2015ISO 14001:2015ISO 45001:2018ISO 630-1:2021IEC 60228ANSA verifiedShorandam Industrial ParkASTM A615 / A370AASHTO M31MISO 9001:2015ISO 14001:2015ISO 45001:2018ISO 630-1:2021IEC 60228ANSA verifiedShorandam Industrial Park

01Who we are

A mill built so that Afghanistan stops importing its reinforcement.

Shams Madina Steel Mill began production in 1402 (2023) and is today one of Afghanistan's best-equipped producers of steel sections. The plant runs two shifts, employs around 600 people directly and supports roughly 1,000 more indirectly.

Our steel goes into housing, markets, townships, and government and private projects across the country. Chemistry is set at the furnace with a spectrometer, and every finished product is pulled, bent and recorded in our physical laboratory before it is allowed to leave the gate.

0+

People employed directly

~1,000 more indirectly

0

ISO standards certified

9001 · 14001 · 45001 · 630-1

0 mm

Largest rebar rolled

From 8 mm up, Grade 60+

0

Shifts per day

Melt shop and rolling line

Registered

Shams Madina Sanati Company with the Standard and Quality Authority of Afghanistan — registration 80907, TIN 9015345433.

02What we make

One melt. A full section list.

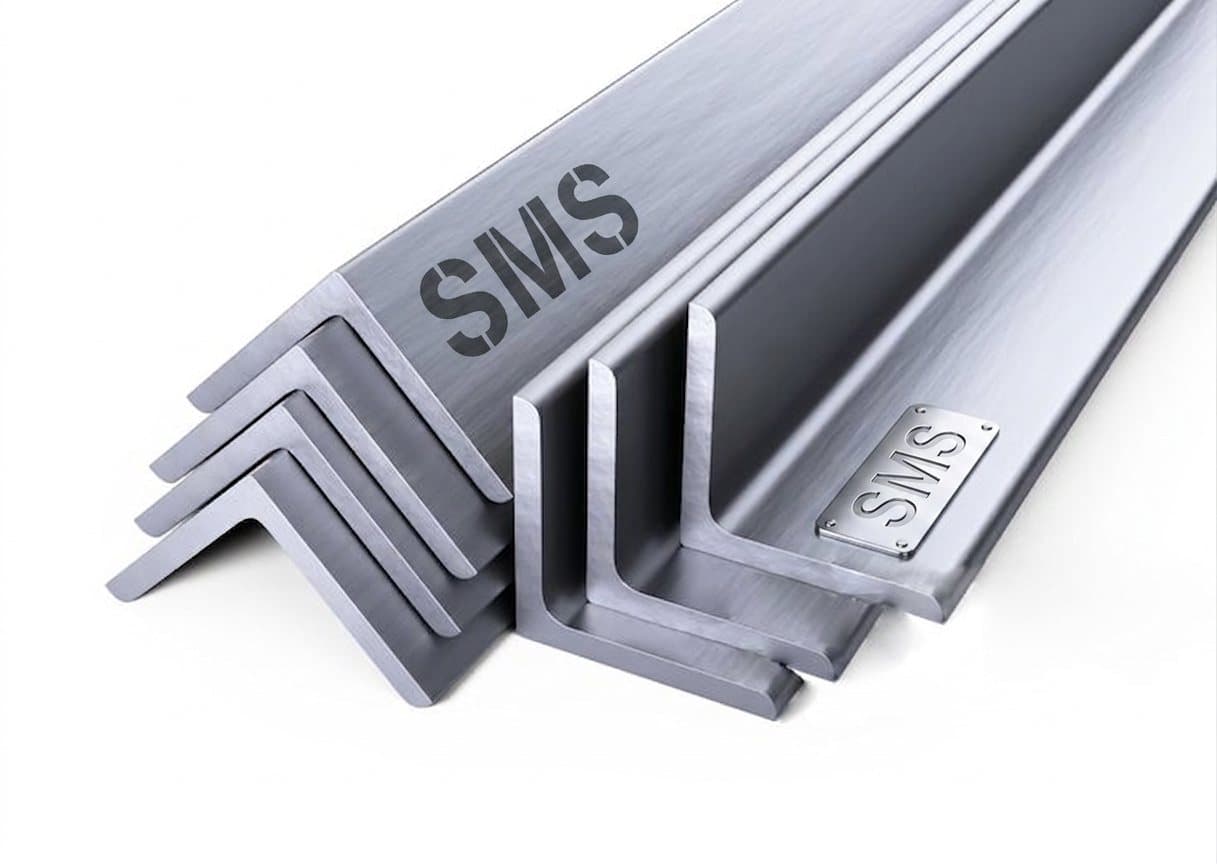
From 8 mm rebar to 150 mm angle iron, nails, mesh and copper cable — every line in the group starts from steel we melt and control ourselves.

All products

03How it is made

From scrap to certificate.

Four stages, each with a hold point. Nothing moves to the next stage until the last one is signed off.

Read the test reports

01How it is made

Charge & spectrometer

Scrap and sponge iron are sorted and charged. During the melt, a spectrometer reads every chemical element in the bath; anything low is added, anything high is burned off before tapping.

  • Spectrometer
  • Charge control
  • Carbon equivalent
  • Scrap steel
  • Sponge iron
  • Ferro-alloys
Melt shopLive

Chemical composition

In spec
C %0.30 / 0.33
S %0.050 / 0.053
P %0.040 / 0.043
Si %0.40 / 0.55
Mn %1.20 / 1.56
CE %0.52 / 0.55

SMSASTM A615
02How it is made

Cast & reheat

Liquid steel is continuously cast into billet, cooled, inspected for surface defects and charged into the reheat furnace at rolling temperature.

  • Continuous casting
  • Surface check
  • Reheat

Caster

Surface check
Reheat furnace
BilletSurface check

03How it is made

Roll & mark

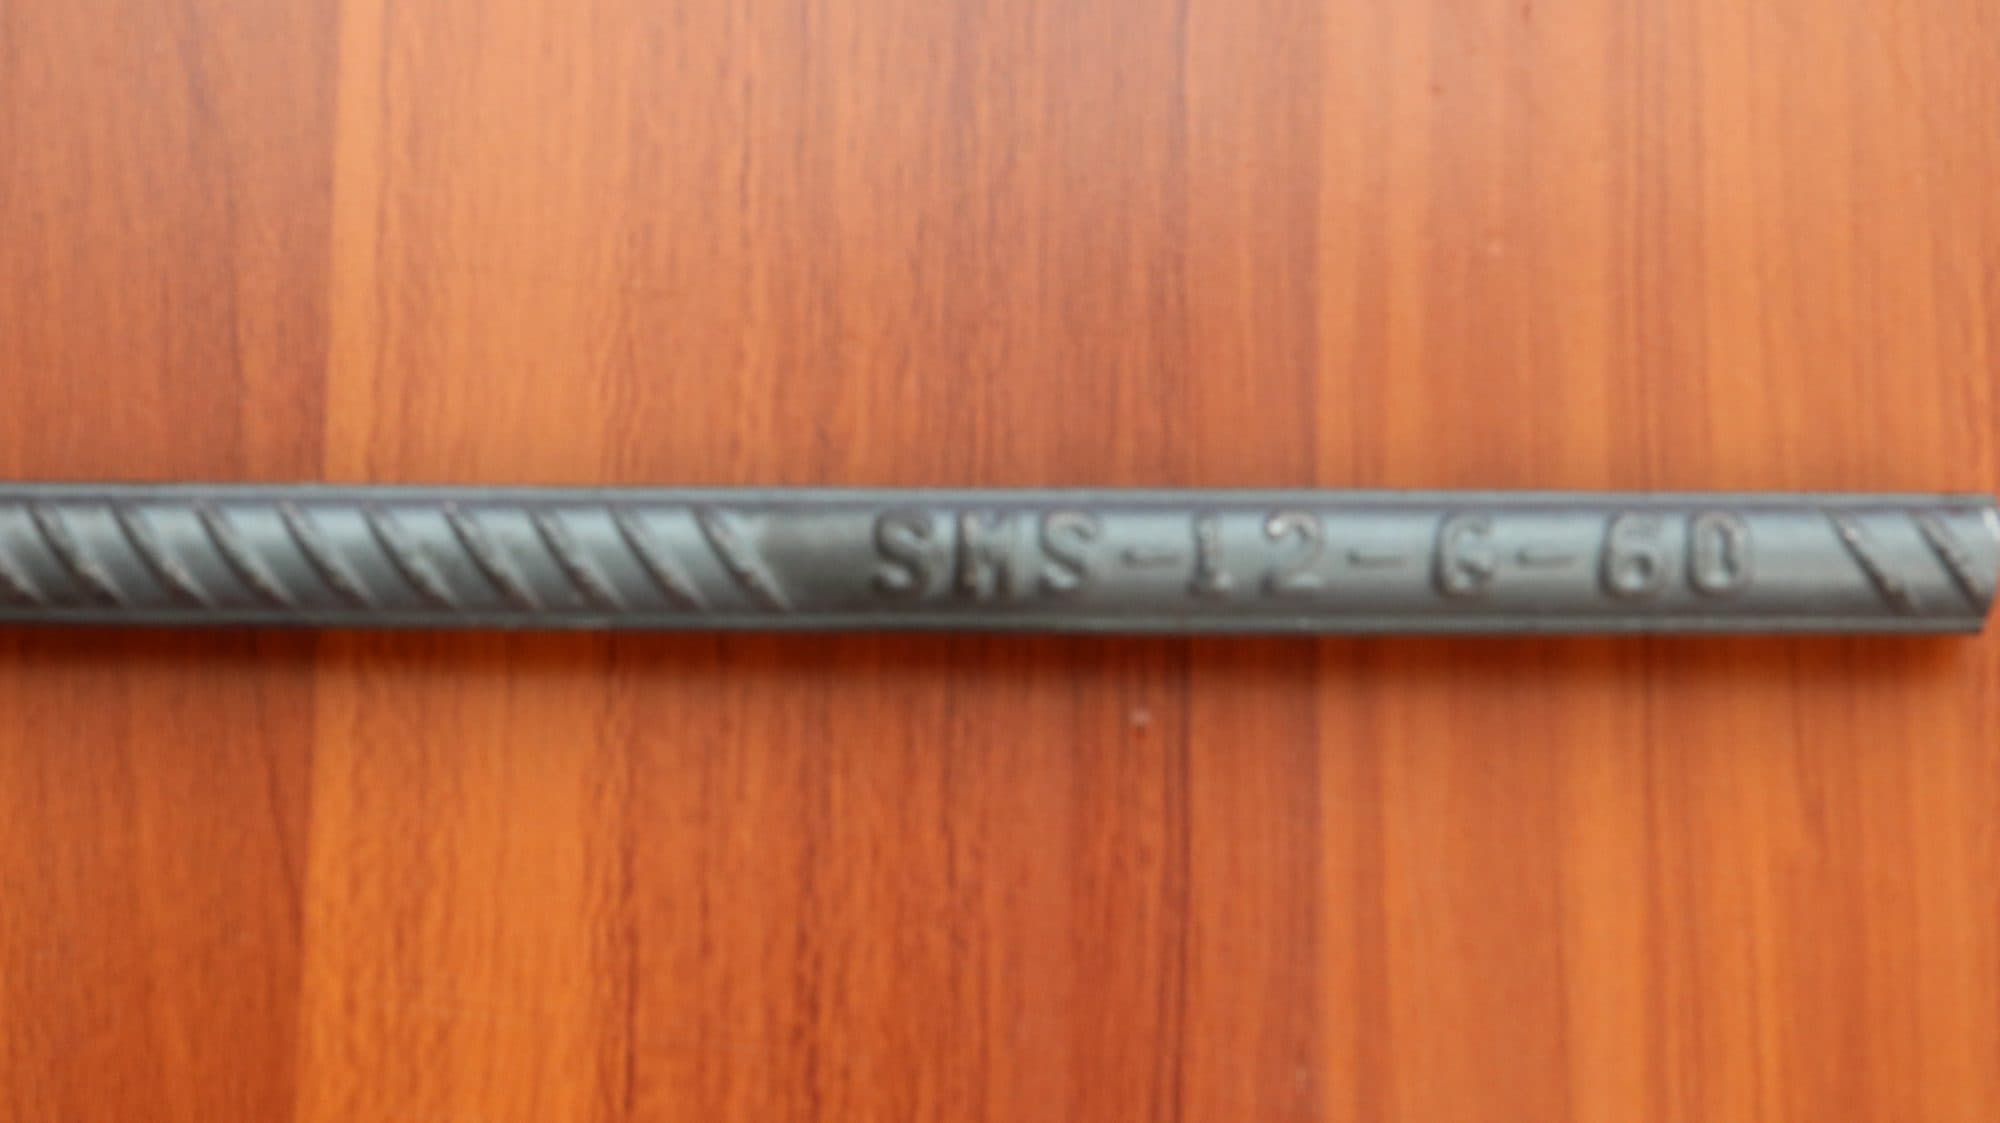
Billet passes through the roughing and finishing stands to final section. The SMS roll mark, grade and diameter are pressed into every bar.

  • Roughing & finishing
  • SMS roll mark
  • 8–32 mm

Stands

Pass line
SMS

Diameter

  • 8 mm
  • 10 mm
  • 12 mm
  • 16 mm
  • 20 mm
  • 25 mm
  • 32 mm

04How it is made

Pull, bend, record

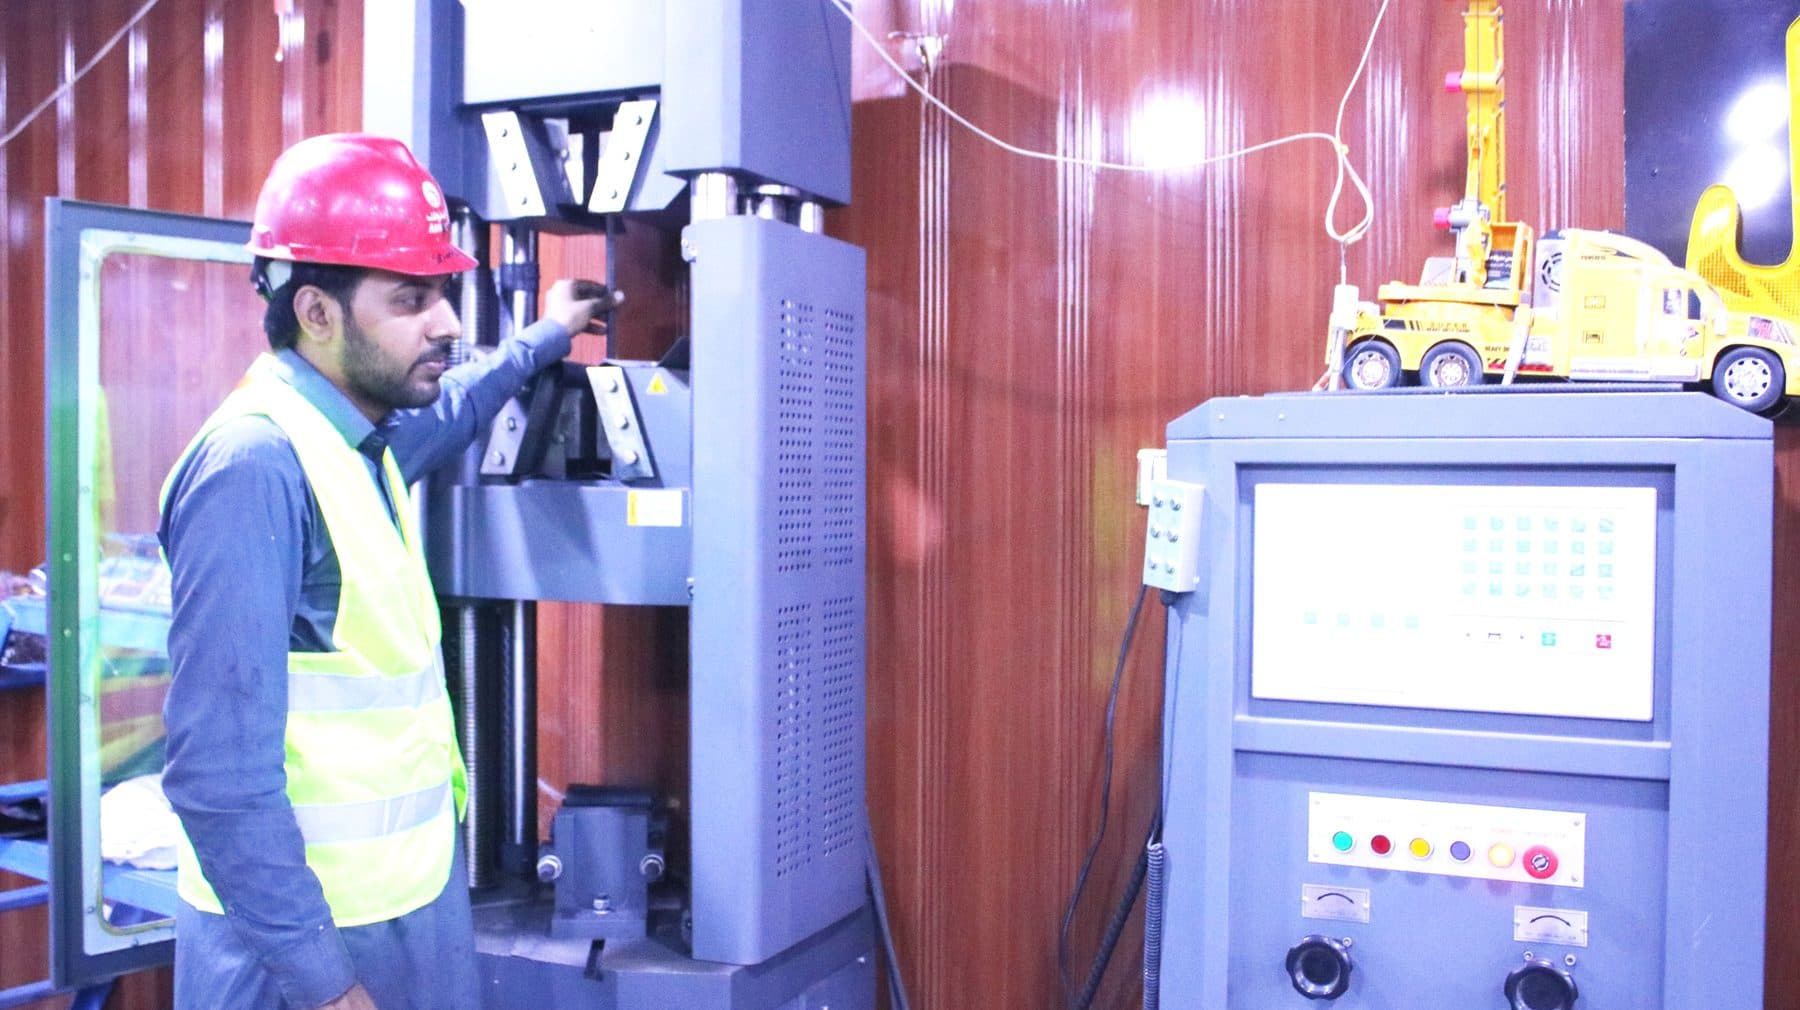
Samples are pulled on the universal testing machine for yield, tensile and elongation, then bent 180°. No product leaves the factory without a passing result on file.

  • Universal testing machine
  • ISO 630-1
  • ASTM A615

Tensile test

Live
180° bend — no cracking

Yield

450 MPa

Tensile

640 MPa

  • Dimensions
  • Weight per metre
  • Tensile & yield
  • Bend test
Elongation 15%Approved for dispatch

04The proof

Numbers, not adjectives.

Our own minimums are set above ASTM A615. These are achieved values from third-party laboratory reports on production bar — Afghan Renewal Geotechnical Laboratory and Real Eiffel Engineering, July 2026.

Yield strength, our minimum

450MPa

ASTM A615 requires 420

Tensile strength, our minimum

640MPa

ASTM A615 requires 620

Elongation, our minimum

15%

ASTM A615 requires 7–9%

180° bend test

Pass

Every diameter, every heat

Two laboratories

Chemical, then physical.

Spectrometer laboratory

During melting, a spectrometer analyses every chemical element in the iron. If an element is below the set limit, the required amount is added; if it is above, it is adjusted down through the technical process. A shortfall or an excess of any element changes the quality of the bar, the girder and everything else, so the melt is tested continuously rather than once.

Physical laboratory

After production, every product is tested on the universal testing machine. For rebar that means grade, tensile resistance, strength, bending, elongation and the other physical characteristics. Sections and other steel products are assessed on size, weight, strength and material quality. Our basic policy is simple: no product is offered to the market without laboratory approval — only material that has passed its tests is allowed to leave the factory.

05Environment

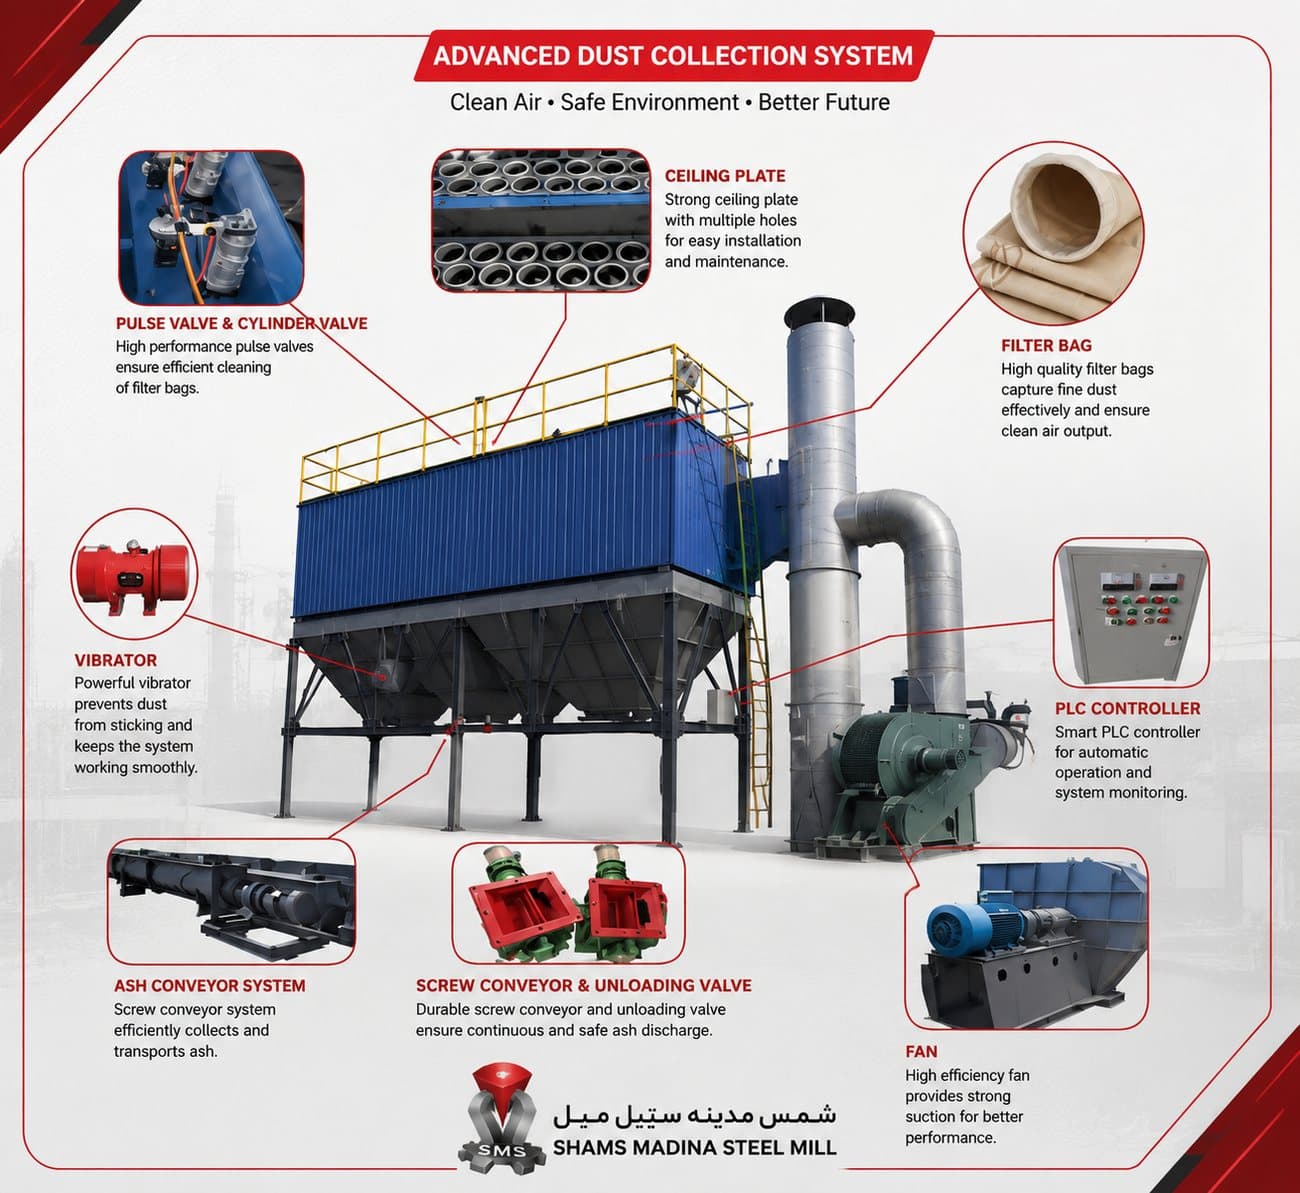
The smoke does not leave the building.

Two large filtration units scrub the melt shop's exhaust. Carbon is captured as powder and stored rather than released — the most advanced carbon-capture installation of its kind in Afghanistan.

200,000

Polluted air filtered per 24 hours

2,000kg

Carbon powder captured per 24 hours

1MW

Power drawn by the filtration system

2

Large filtration units installed

06Certification

Audited, not self-declared.

Four management-system and product standards, certified by UK Certification & Inspection and valid to January 2028.

View certificates

ISO 9001:2015

Quality Management System

Cert. no.
UQ-2025012221
Valid to
21 January 2028

ISO 14001:2015

Environmental Management System

Cert. no.
UQ-2025012222
Valid to
21 January 2028

ISO 45001:2018

Occupational Health & Safety

Cert. no.
UQ-2025012223
Valid to
21 January 2028

ISO 630-1:2021

Structural Steels — Part 1

Cert. no.
UQ-2025012224
Valid to
21 January 2028

07The plant

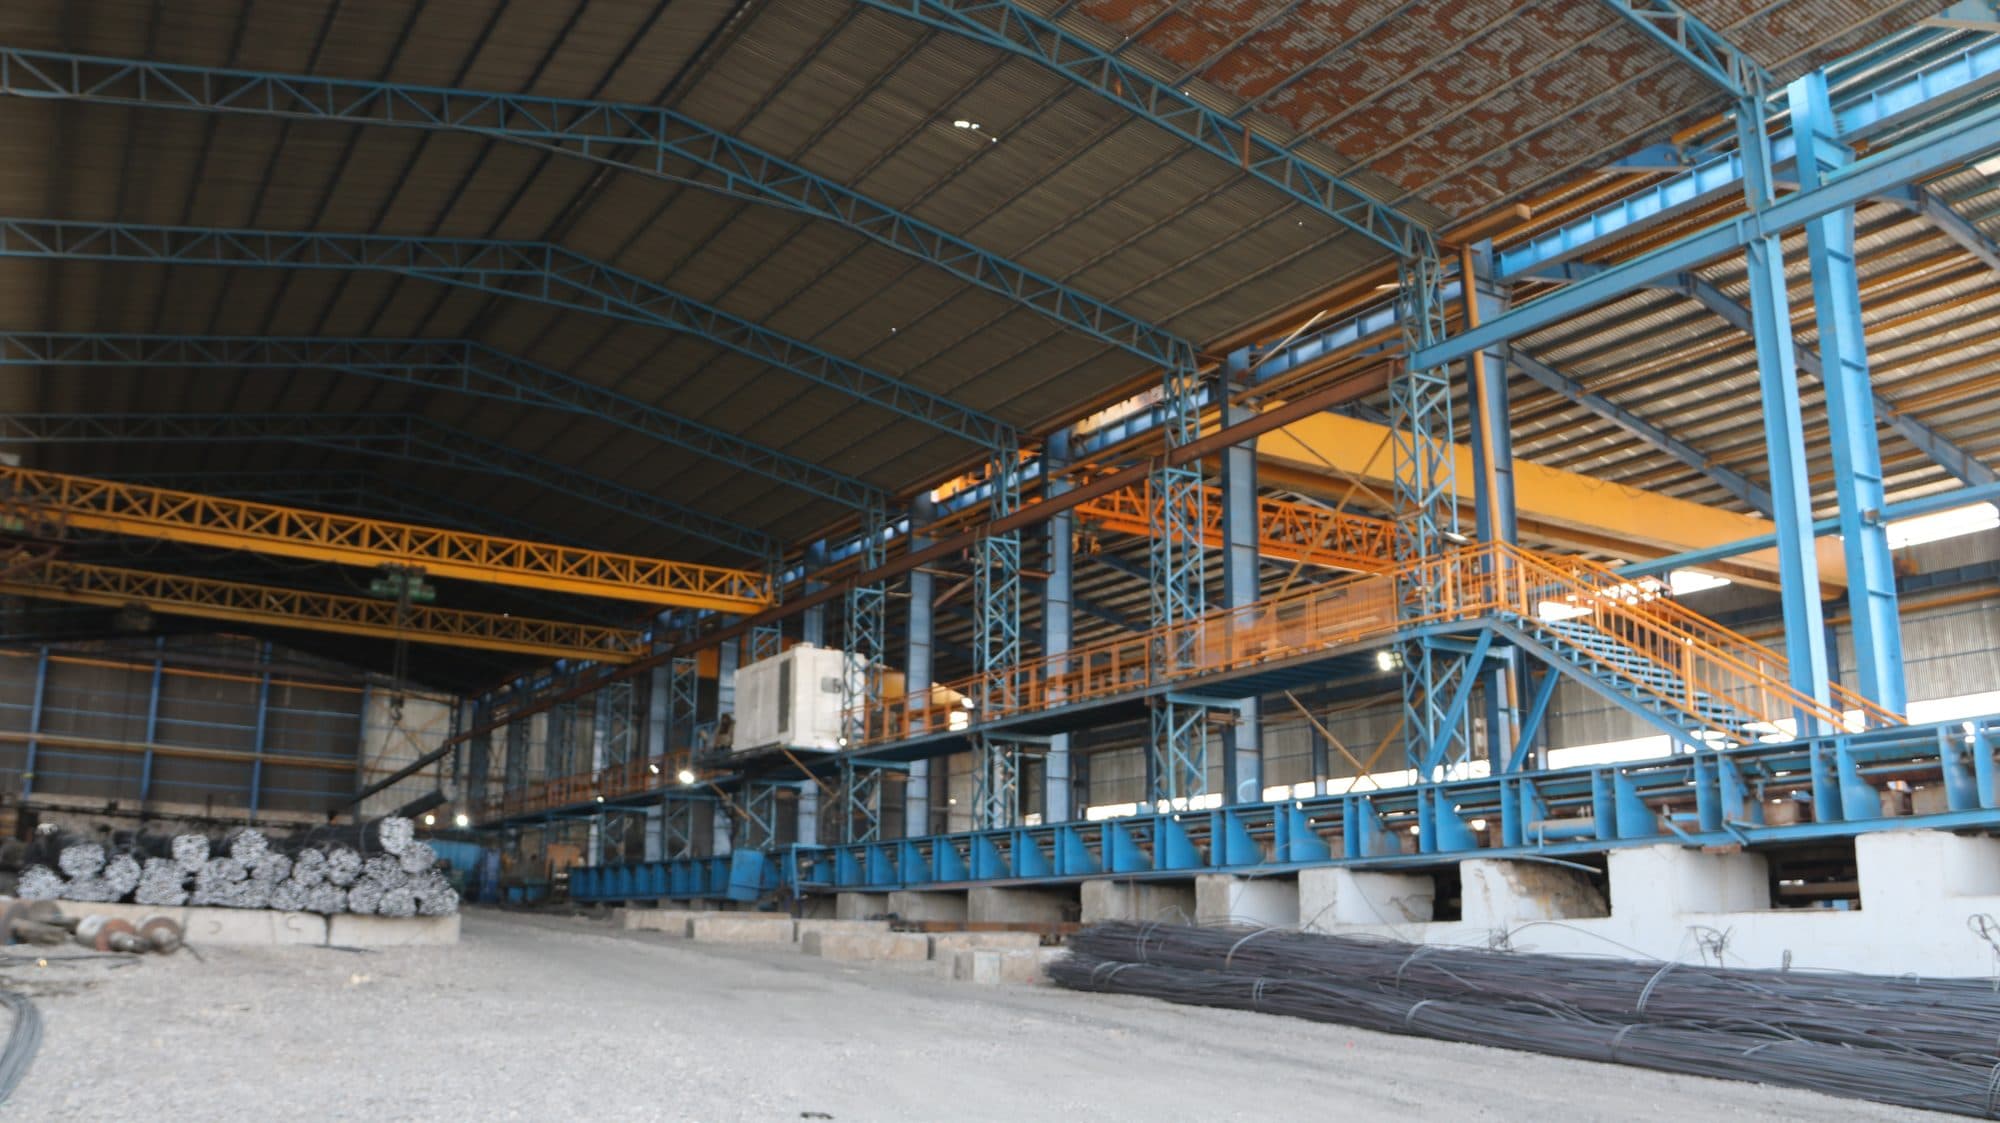
Shorandam Industrial Park, Kandahar.

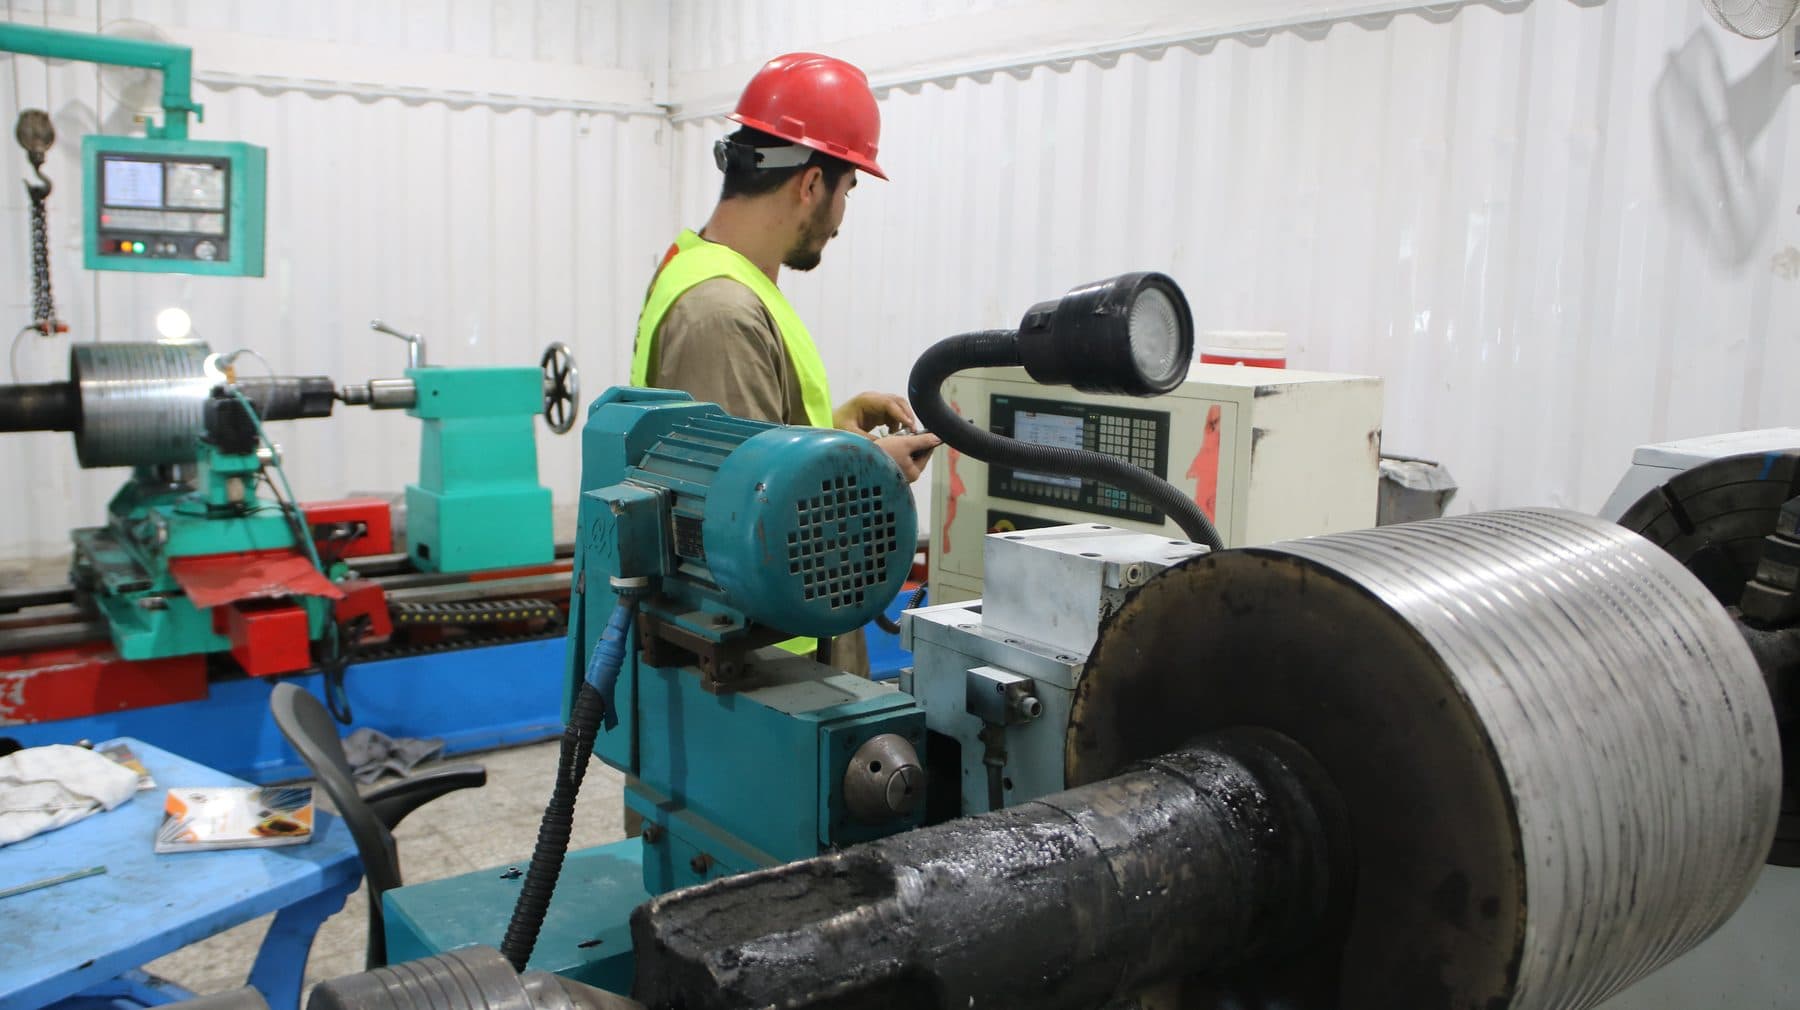
A melt shop, a rolling line, a section mill, a nail and mesh plant, a copper cable factory and two laboratories — on one site, under one management system.

Get in touch

Tell us the tonnage. We will tell you the lead time.

Send your bar schedule, diameters and delivery point. Quotes go out with a copy of the latest mill test certificate for the sizes you need.